Pre-Shipment Inspection Checklist for Tools, Equipment, and Auto Parts
A practical framework for verifying quantity, quality, packaging, documentation, and shipment readiness before the balance is paid.
Once goods have been loaded and dispatched, correcting a manufacturing or packaging problem becomes slower and more expensive. A structured pre-shipment inspection gives B2B buyers an opportunity to verify the order while it is still at the supplier’s facility and corrective action remains practical.
Inspection is not a substitute for supplier qualification, clear specifications, approved samples, or a strong purchase contract. It is the final control point in a wider procurement process. The most useful inspection plan is written before production starts and linked to objective acceptance criteria rather than a general request to “check quality.”
The required depth depends on product risk. A shipment of hand tools, a batch of electric pumps, a generator order, and safety-related automotive components should not all receive the same inspection. Order value, technical complexity, regulatory requirements, failure consequences, and the supplier’s performance history should determine the level of control.
Define the Inspection Plan Before Production
A pre-shipment inspector can only verify requirements that have been clearly defined. The inspection brief should refer to the signed purchase order, current drawings, approved sample, packaging artwork, labels, manuals, test methods, and any destination-market requirements.
Before scheduling the visit, confirm that production is complete and most goods are packed. If the order is inspected too early, the sample may not represent the finished shipment. If the inspection is scheduled after the cargo is sealed or transferred to a port warehouse, access and corrective action may be limited.
The plan should state:
- Product references, models, variants, and order quantities.
- Inspection location and expected production-completion level.
- Sampling method and sample size for each product group.
- Critical, major, and minor defect definitions.
- Measurements, tests, and equipment required.
- Approved tolerances and acceptance criteria.
- Packaging, labeling, barcode, and documentation requirements.
- Actions required when the result is passed, pending, or failed.
Core Pre-Shipment Inspection Checks
The inspector should reconcile the goods with the purchase order and packing list. Verify model numbers, part references, sizes, colors, ratings, accessories, and country-of-origin marking where required. Count finished units, export cartons, pallets, and any spare-parts or promotional items.
Mixed orders deserve special attention. A correct total quantity can still hide shortages in one variant and excess stock in another. Carton markings should allow the buyer to identify contents without opening every package.
Visual checks should be product-specific and consistent with the approved reference. Typical defects include cracks, corrosion, poor coating, sharp edges, loose fasteners, oil leakage, damaged connectors, misaligned assemblies, contamination, inconsistent finish, and evidence of rework.
For retail or distributor stock, presentation also matters. Scratched housings, mismatched colors, damaged cases, or irregular printing may make a technically functional product commercially unacceptable.
Measure the characteristics that affect fit, performance, safety, or installation. Depending on the product, this may include dimensions, thread type, cable length, voltage, frequency, power rating, pressure range, flow direction, material grade, weight, tolerances, or compatible vehicle application.
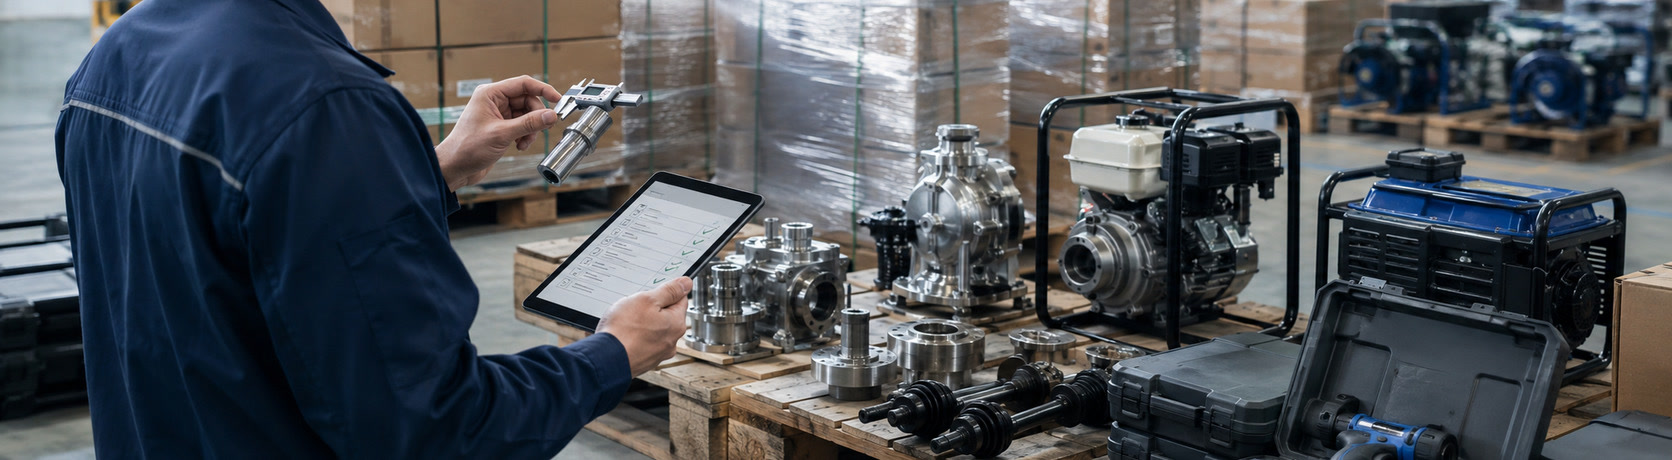
Inspection equipment should be suitable and calibrated where accuracy is material. Measurement points and test methods should match the drawing or contract; otherwise, the buyer and supplier may obtain different results from the same item. Functional checks confirm that sampled products operate as intended. Tools may be run under a defined load. Pumps may be checked for direction, leakage, noise, and agreed performance points. Generators may require start-up, output, control-panel, protection, and accessory checks. Automotive parts may need fitment, electrical continuity, dimensional, pressure, or material tests.
A short factory demonstration is not automatically equivalent to a laboratory or compliance test. The inspection report should distinguish between an on-site functional check, a supplier record review, and testing performed by an accredited laboratory. Packaging must protect the goods throughout handling, storage, and international transport. Review individual product packaging, internal cushioning, moisture protection, master cartons, pallet condition, strapping, corner protection, and crate construction. Heavy or irregular equipment should be secured so that movement does not damage the product or create a handling risk.
Verify model labels, warnings, manuals, barcodes, carton marks, gross and net weights, package dimensions, and any language or recycling information required by the destination. Packaging errors often affect customs clearance, warehouse receiving, and retail readiness even when the product itself is correct. The inspector should compare physical markings with the draft packing list and other shipment documents. Where relevant, record serial numbers, lot numbers, production dates, material batches, and test-report references. Photographs should show the product, labels, carton marks, packaging configuration, and any observed defects.
Traceability is particularly important when the buyer may need to isolate a defective batch, make a warranty claim, or demonstrate product origin. A generic certificate that cannot be connected to the inspected shipment provides limited assurance.
Sampling and AQL: What Buyers Should Understand
Most large orders cannot be inspected unit by unit. Acceptance sampling selects a defined number of units from a lot and compares the findings with agreed acceptance criteria. ISO 2859-1:2026 provides sampling schemes for inspection by attributes indexed by acceptance quality limit, commonly referred to as AQL.
AQL should not be treated as a promise that the shipment contains no defects. It is part of a statistical acceptance system. The contract should define the inspection level, lot structure, defect categories, and acceptance or rejection numbers. Safety-critical characteristics may require stricter controls or complete inspection rather than routine sampling.
Samples should be selected across different cartons, pallets, production times, and variants. Allowing the supplier to present only specially prepared units undermines the purpose of random sampling.
- Dimensions, material, surface finish, and assembly quality.
- Torque, cutting, clamping, fastening, or other agreed functional checks.
- Battery, charger, plug, voltage, accessories, and case contents for power tools.
- Sharp-edge protection, corrosion prevention, and retail packaging.
- Nameplate data and consistency with the ordered configuration.
- Start-up, controls, noise, leakage, vibration, and visible workmanship.
- Connections, hoses, fittings, guards, wheels, handles, and included spare parts.
- Manuals, wiring information, test records, and shipping protection.
- Exact part reference, vehicle application, side, position, and supersession status.
- Critical dimensions, connectors, mounting points, materials, and finish.
- Lot or serial traceability and consistent packaging labels.
- Additional validation for braking, steering, suspension, airbag, wheel, fuel, or other safety-related components.
A failed inspection should trigger a controlled response, not an automatic shipment release or an immediate argument about blame. The report should identify affected references, defect category, quantity found, photographs, measurements, and the clause or specification that was not met.
Possible actions include sorting the lot, reworking affected units, replacing products, correcting labels or packaging, repeating tests, or producing a new batch. The supplier should provide a corrective-action plan that addresses both the observed defect and its cause. Reinspection should focus on the corrected issue while still confirming that rework has not introduced a new problem. Final payment and shipment authorization should follow the contractually agreed release process.
A Practical Shipment-Release Workflow
- Confirm that production and packing have reached the required completion level.
- Issue the latest inspection brief and controlled reference documents.
- Select samples across the order rather than from supplier-prepared units.
- Check identity, quantity, workmanship, dimensions, function, packaging, and records.
- Classify defects and compare results with the agreed acceptance criteria.
- Review the report with procurement, quality, and logistics stakeholders.
- Close corrective actions and arrange reinspection when required.
- Approve shipment only after commercial and quality release conditions are satisfied.
Final Pre-Shipment Release Checklist
The value of inspection increases when results are used beyond a single shipment. Track recurring defects, documentation errors, response times, and corrective-action quality. This creates a supplier performance record that can guide future order volumes, audit frequency, and sourcing decisions.
Cropinside coordinates supplier communication, product requirements, export documentation, inspection support, freight, and delivery monitoring for international B2B orders across tools, equipment, automotive products, and industrial spare parts.
Speak with our Experts